 Tiếng Việt
 English
 日本語

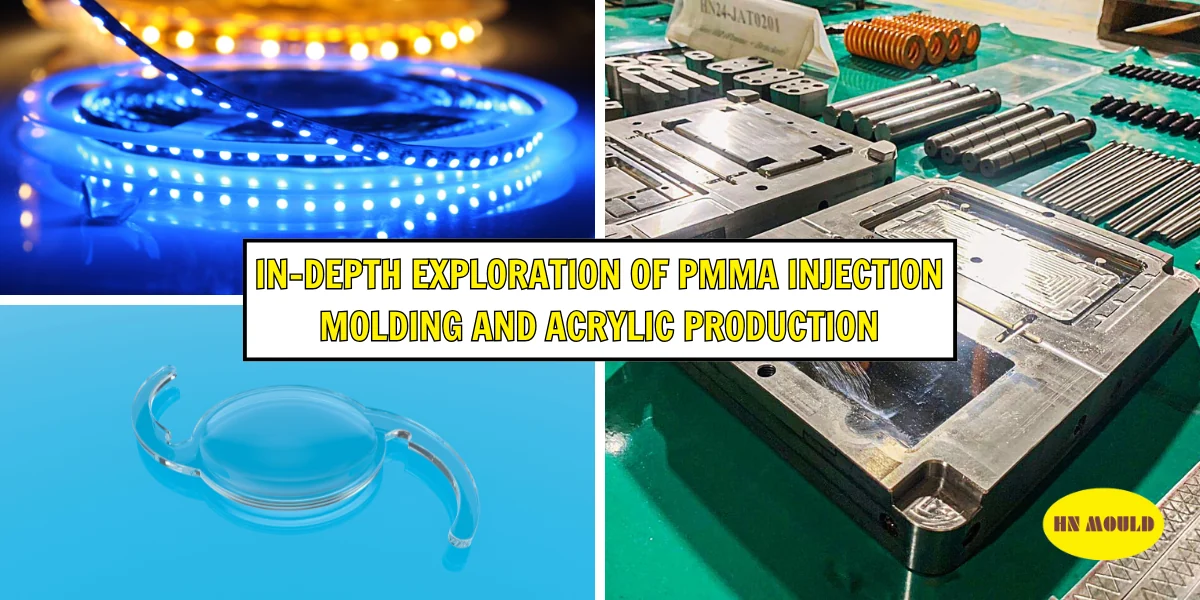
PMMA (polymethyl methacrylate), commonly called acrylic, is a thermoplastic considered when a project requires controlled transparency, surface appearance or light transmission. Injection-molding results do not come from one universal process window. They must be reviewed against the selected resin grade, supplier technical data, part geometry, mold design, machine, trial conditions and inspection criteria.
HA NOI MOULD TECHNOLOGY COMPANY LIMITED (HANOI MOULD) uses customer 2D/3D data, material requirements and acceptance criteria to review DFM, mold design, trials and correction items. This guide summarizes the information and engineering checks needed before requesting a PMMA/Acrylic injection mold quotation.
What is PMMA and why does the grade matter?
PMMA is a material family rather than a single specification. General-purpose, optical, impact-modified, UV-stabilized, colored and recycled-content grades can differ in viscosity, optical behavior, shrinkage, strength and processing guidance. The exact grade and its technical data sheet (TDS) should therefore be confirmed before the mold concept or trial plan is finalized.
Input data for a PMMA injection mold
- 2D drawings, 3D data or an approved product sample for engineering review.
- Resin grade, TDS, color, permitted recycled-content ratio and traceability requirements, if applicable.
- Light transmission, haze, color, gloss, scratch limits and critical appearance zones.
- Product operating conditions, including load, temperature, chemicals, UV exposure and assembly interfaces.
- Expected volume, cavity count, preferred gate concept and automation requirements, if any.
- Inspection method, limit samples, required documents, packaging and project schedule.
DFM checks for PMMA parts
PMMA DFM needs to consider filling behavior and visible quality at the same time. Key review items include:
- Wall thickness and transitions: reduce abrupt changes that may create stress, sink or optical variation.
- Radii and draft: support flow and lower release force on appearance-sensitive surfaces.
- Gate location: review gate vestige, flow direction, weld lines and critical viewing areas.
- Venting: place vents according to the expected flow path and end-of-fill locations.
- Cavity surface: define the required finish, polishing zones and surface-protection rules.
- Cooling and ejection: review temperature balance, distortion, ejector marks, cracking and scratches during release.
Use the injection mold DFM checklist to organize the required information before design.
Process setup and mold trials
Drying, melt and mold temperatures, injection speed, holding conditions and cooling time should start from the supplier guidance for the selected grade. The settings then need to be adjusted for the machine, part and mold-trial results. One fixed temperature or pressure range should not be applied to every PMMA project.
Each trial record should identify the material, drying status, machine configuration, molding conditions, mold changes and inspection results. Trial parts are checked against drawings, appearance criteria and agreed assembly conditions before the next correction loop. See the mold inspection and validation process.
Common PMMA molding defects to review
- Silver streaks, bubbles or haze: review material condition, moisture, heat history and trapped gas.
- Burn marks or short shots: check venting, gate position, flow path and filling conditions.
- Weld lines or optical variation: review flow-front meeting points, temperature, speed and viewing-zone requirements.
- Warpage or dimensional variation: check wall thickness, cooling balance, packing, stress and measurement conditions.
- Cracks, scratches or ejector marks: review draft, polishing, ejection design, part handling and packaging.
Frequently asked questions
Can one process window be used for every PMMA grade?
No. Each grade has its own supplier guidance and process behavior. Initial settings should follow the selected grade’s TDS and then be confirmed through mold trials.
How should optical requirements be specified?
Define the viewing area, color, transparency or haze, gloss or texture, acceptable defects, limit samples and inspection method when these are available.
What data is needed for a PMMA mold review?
Provide 2D/3D data or a product sample, grade/TDS, volume, appearance requirements, operating conditions, inspection criteria and project timing. See the injection mold RFQ data checklist.


